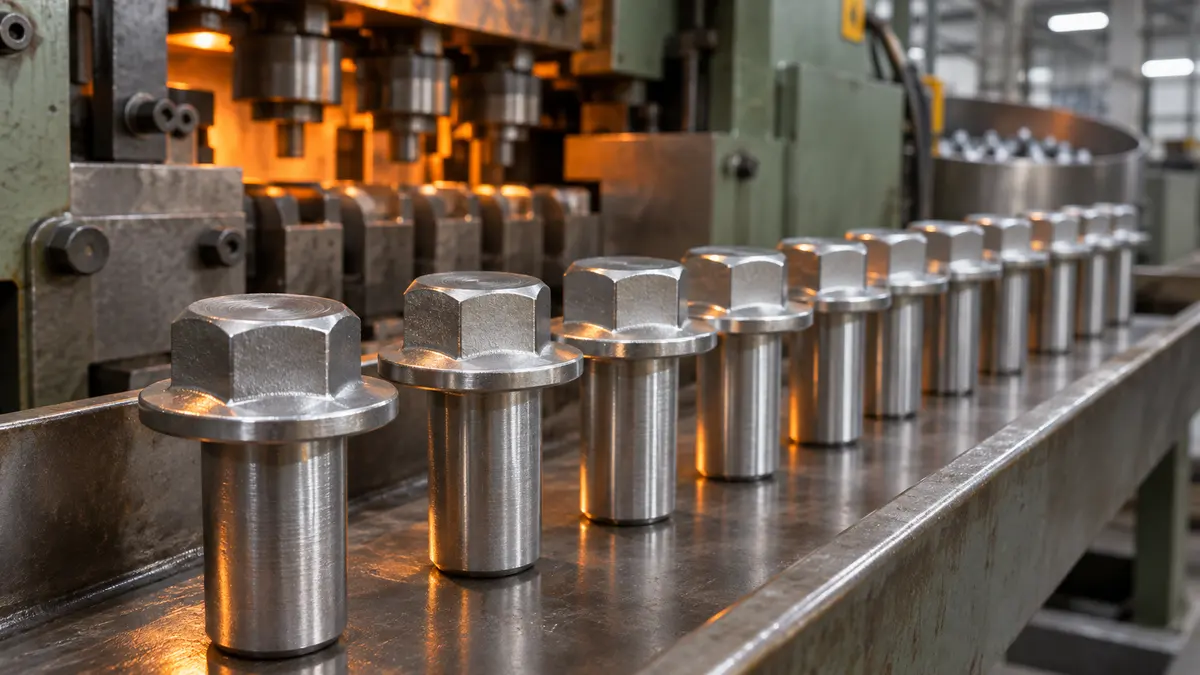
Six process stations
The same bolt from wire to finished part, left to right.
Wire preparation
Incoming wire is sampled for chemistry and tensile strength, then drawn and spheroidize annealed so it forges easily.
- Equipment
- 4 wire drawing machines, annealing furnace (outsourced)
- Control
- Wire diameter tolerance ±0.03 mm
Cold forging
Wire is cut to slugs and struck by several dies in sequence. Head and shank form in one pass with no cutting and little waste.
- Equipment
- 9 multi station presses, 5 two die three blow presses
- Control
- Head diameter ±0.1 mm, checked every 2 hours
Thread rolling
Threads are rolled, not cut, so the grain flow stays intact and thread strength is higher.
- Equipment
- 12 thread rollers
- Control
- Go and no go gauge every lot, class 6g
Heat treatment
Continuous belt furnace quench and temper for grades 8.8 to 12.9.
- Equipment
- 2 continuous belt furnaces
- Control
- Hardness sampled per load, grade 10.9 at HRC 32 to 39
Surface finish
Plating is done at partner lines (outsourced). Our staff supervise and sample.
- Equipment
- Outsourced lines: zinc, zinc nickel, Dacromet
- Control
- Coating thickness and salt spray hours per customer spec
Inspection and packing
Optical sorters check appearance and size. After manual recheck, parts are packed by lot.
- Equipment
- 3 optical sorters, 2 profile projectors
- Control
- 100 percent check before shipping, lot records kept 5 years
Equipment list
Auditors usually start here. Outsourced items are marked.
| Equipment | Qty | Specification | Use |
|---|---|---|---|
| Multi station cold former | 9 | three die four blow to four die five blow, 80 to 300 t | Bolts, flange bolts, special forgings |
| Two die three blow former | 5 | 60 to 120 t | Small screws, nuts |
| Thread roller | 12 | Flat die and roller type, M2 to M20 | Thread rolling |
| Continuous belt furnace | 2 | Quench and temper, protective atmosphere | Heat treatment |
| Wire drawing machine | 4 | Wire 3 to 24 mm | Wire preparation |
| Optical sorter | 3 | Appearance and size, 200 to 400 pcs per minute | Final inspection |
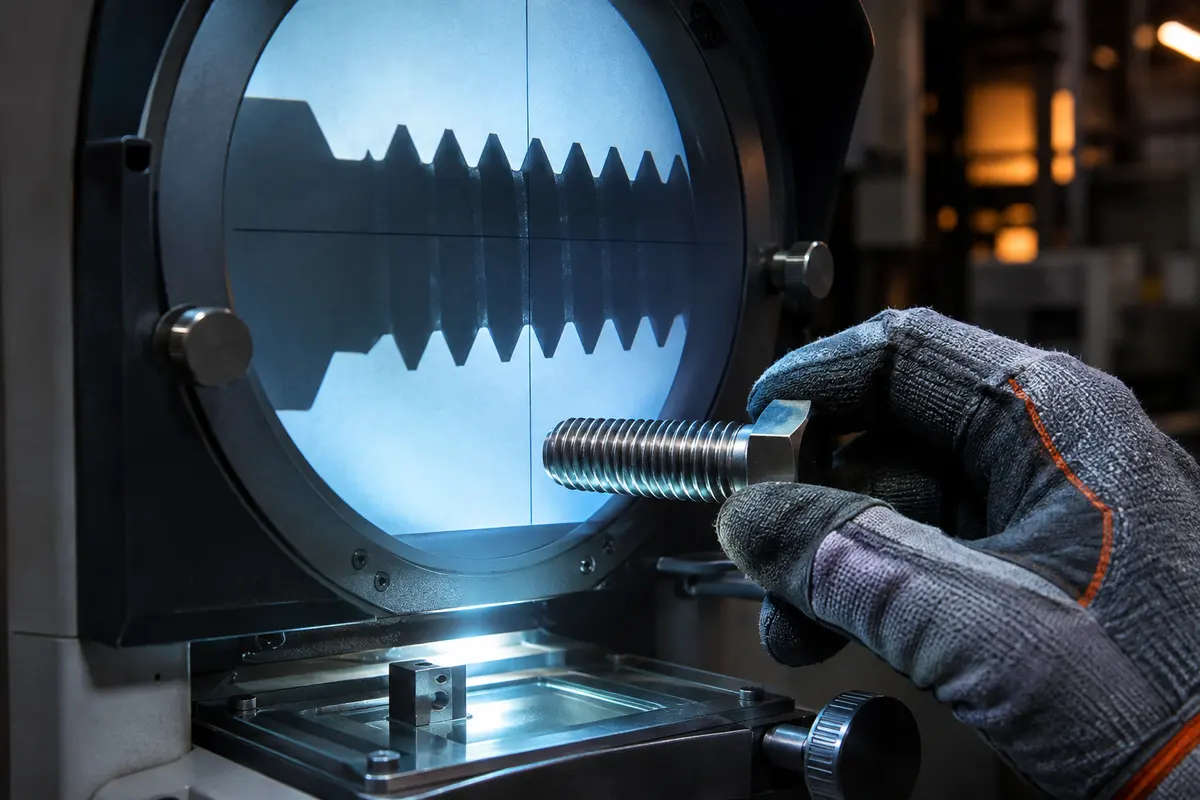
| Profile projector | 2 | 10x to 50x magnification | Thread and head profile |
| Rockwell hardness tester | 2 | HRC / HRB | Heat treatment check |
| Universal tester | 1 | Up to 600 kN | Tensile and wedge load |
| Salt spray chamber | 1 | Neutral salt spray per ISO 9227 | Coating corrosion test |
| Plating line (outsourced) | Partner | Zinc, zinc nickel, Dacromet | Surface finish |
Inspection plan
- Each wire lot
Incoming
Chemistry, diameter, tensile strength.
- Every start up
First article
Full dimension check, released only after sign off.
- Every 2 hours
In process
Head diameter, thread gauge, appearance, logged on the lot card.
- Every furnace load
After heat treatment
Hardness, tensile, decarburization.
- 100%
Before shipping
Optical sorting plus manual recheck.
- Lot no.
Traceability
From wire heat number to shipping note, kept 5 years.
Certificates and reports
All demo data, not real certificates, and no certification body marks are used.
| Certification | Scope | Certificate no. | Valid until |
|---|---|---|---|
| ISO 9001 (demo) | Design and manufacture of cold forged fasteners | DEMO-QMS-0001 | 2027/06 |
| IATF 16949 (demo) | Manufacture of automotive fasteners | DEMO-AUTO-0002 | 2027/03 |
| ISO 14001 (demo) | Environmental management system | DEMO-EMS-0003 | 2027/09 |
Material certificate sample (EN 10204 3.1 format)DEMO
- Customer
- DEMO BUYER GmbH
- Part
- Hex flange bolt M8 x 1.25 x 30
- Lot no.
- LF-241109-03
- Wire heat no.
- H-88231
- Chemistry %
- C 0.36 Mn 0.72 Cr 1.02 Mo 0.19
- Hardness
- HRC 35
- Result
- Pass